


Quality Ultra Pure Water System Manufacturers Meet Growing Demand for High-Purity Water Solutions
Time:
Mar 20,2025
The demand for ultra-pure water is on the rise across industries such as pharmaceuticals, semiconductors, power generation, and healthcare, where water quality is critical for operational success. Quality ultra pure water system manufacturers are playing a vital role in meeting this demand, providing advanced systems that deliver water with exceptionally low levels of impurities. These manufacturers are recognized for their ability to combine cutting-edge technology with reliable performance, ensuring that industries have access to the high-purity water they require.
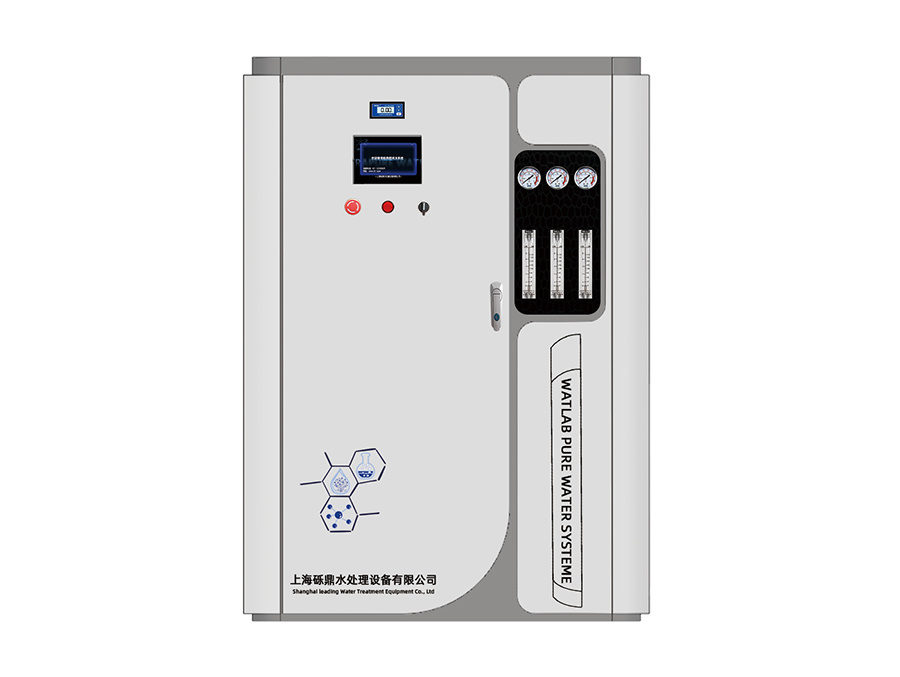
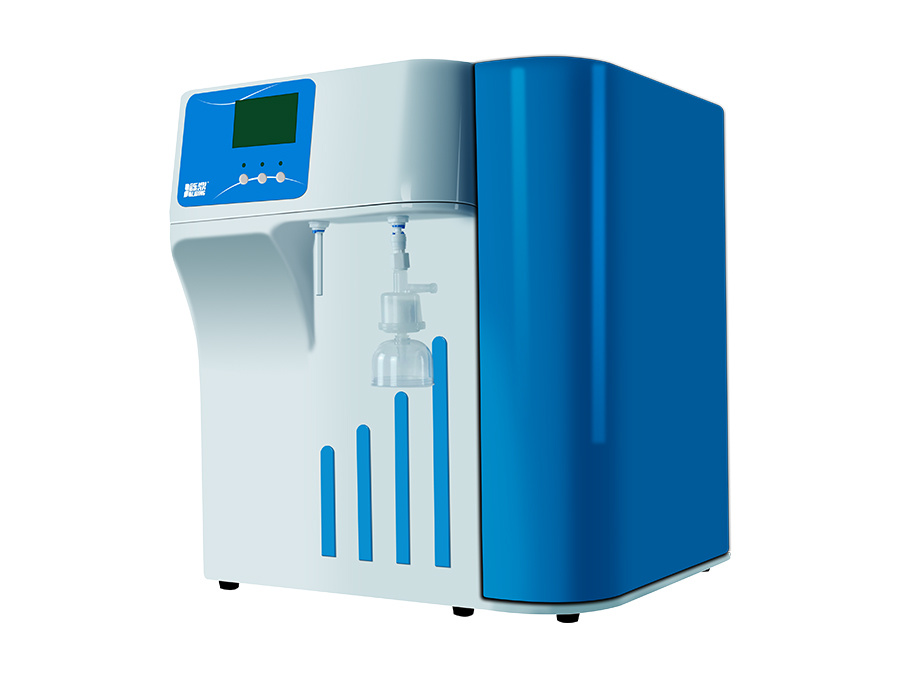
Quality ultra pure water system manufacturers design and produce systems that remove contaminants such as ions, particles, bacteria, and organic compounds to achieve water purity levels measured in parts per billion (ppb) or even parts per trillion (ppt). These systems typically incorporate multi-stage processes, including reverse osmosis, deionization, and ultrafiltration, to ensure consistent and reliable results. By offering customizable solutions, quality ultra pure water system manufacturers cater to the specific needs of different industries, whether for laboratory research, pharmaceutical production, or semiconductor manufacturing.
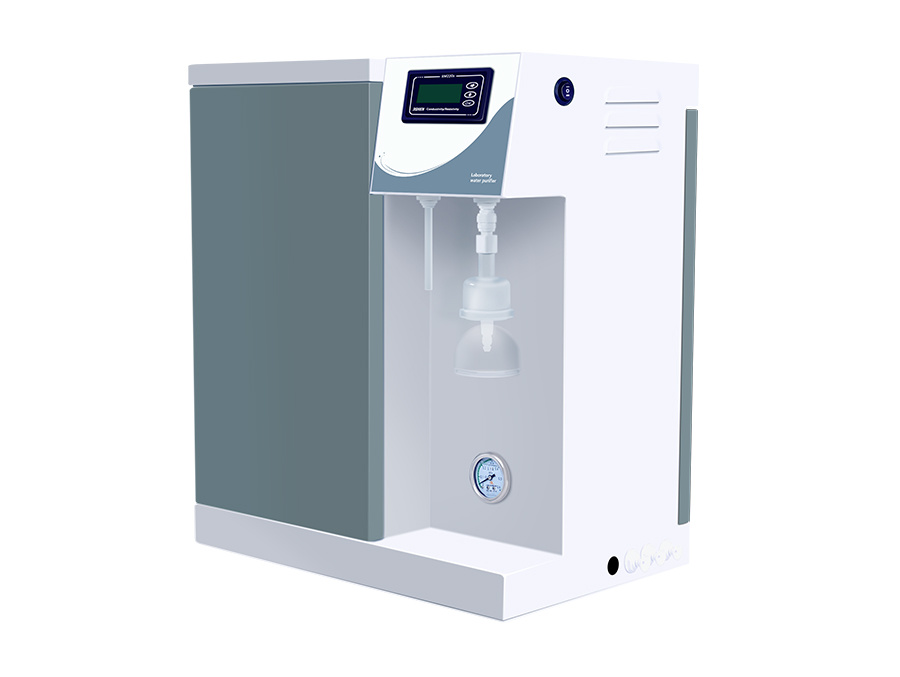
One of the key advantages of working with quality ultra pure water system manufacturers is their focus on innovation and efficiency. Modern ultra-pure water systems are designed to minimize water waste and energy consumption, aligning with the global trend toward sustainability. Many manufacturers also integrate advanced monitoring and control technologies, allowing users to track water quality in real-time and optimize system performance. This combination of precision and sustainability has made quality ultra pure water system manufacturers a preferred choice for industries prioritizing both performance and environmental responsibility.
The global market for ultra-pure water systems is experiencing significant growth, driven by the expanding semiconductor and pharmaceutical sectors, as well as increasing regulatory requirements for water quality. Quality ultra pure water system manufacturers are well-positioned to meet this demand, thanks to their ability to scale production and deliver systems that meet stringent industry standards. Their commitment to research and development ensures that their products remain at the forefront of water purification technology, providing reliable solutions for even the most demanding applications.
Another factor contributing to the popularity of quality ultra pure water system manufacturers is their emphasis on after-sales support and service. Many manufacturers offer comprehensive maintenance packages, training programs, and technical assistance to ensure that their systems operate at peak efficiency throughout their lifecycle. This level of support not only enhances customer satisfaction but also reduces downtime and operational costs for businesses.
As industries continue to prioritize high-purity water for their processes, the demand for advanced ultra-pure water systems is expected to grow. Quality ultra pure water system manufacturers are set to play a crucial role in meeting this demand, thanks to their combination of innovative technology, reliability, and customer-focused services. With ongoing advancements in water purification techniques, these manufacturers are likely to remain key players in the global market.
RELATED NEWS
Tel:
E-mail:
Ask For A Quick Quote
We will contact you within one working day. Please pay attention to your email