


Unlocking the Benefits of Ultra Pure Water Equipment in Industrial Applications
Time:
Mar 19,2025
Unlocking the Benefits of Ultra Pure Water Equipment in Industrial Applications
Table of Contents
1. Introduction to Ultra Pure Water Equipment
2. The Importance of Ultra Pure Water in Industrial Applications
2.1. Industries That Benefit from Ultra Pure Water
2.2. Role of Ultra Pure Water in Compliance and Safety
3. Types of Ultra Pure Water Equipment
3.1. Reverse Osmosis Systems
3.2. Deionization Units
3.3. Ultraviolet (UV) Treatment Systems
4. Advantages of Using Ultra Pure Water Equipment
4.1. Enhanced Product Quality
4.2. Increased Operational Efficiency
4.3. Cost Savings in the Long Run
5. Selecting the Right Ultra Pure Water Equipment
5.1. Assessing Your Water Quality Needs
5.2. Evaluating System Compatibility and Future Scalability
6. Installation and Maintenance Considerations
6.1. Key Installation Tips
6.2. Regular Maintenance Best Practices
7. Case Studies: Success Stories in Ultra Pure Water Implementation
8. Frequently Asked Questions
9. Conclusion
1. Introduction to Ultra Pure Water Equipment
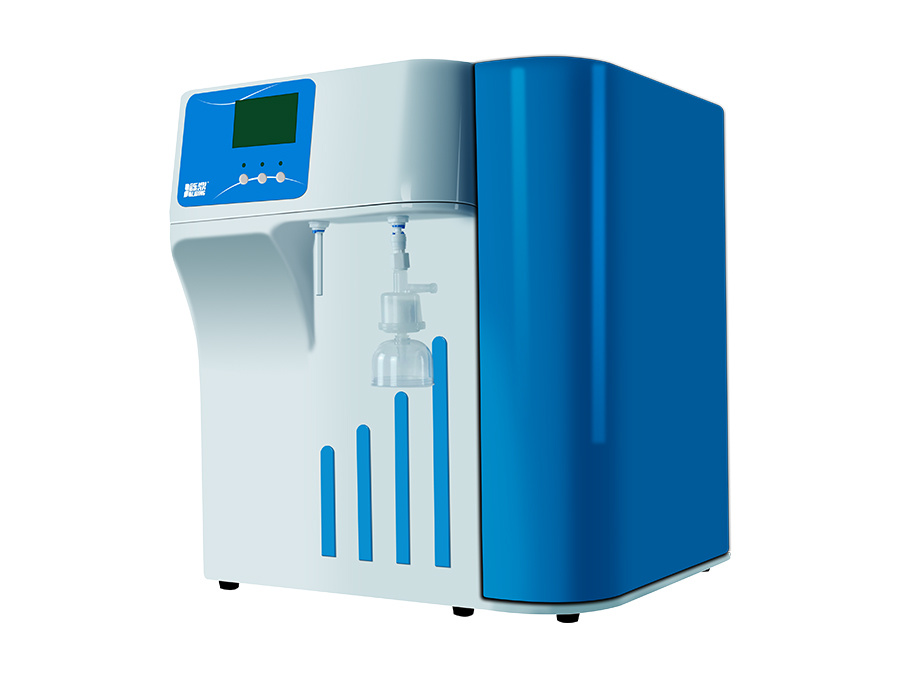
In the realm of industrial applications, the demand for water quality has never been more critical. **Ultra pure water equipment** plays a vital role in ensuring that industries have access to the highest quality water necessary for their operations. This category of equipment is specifically designed to remove impurities and contaminants, delivering water that meets stringent quality standards.
2. The Importance of Ultra Pure Water in Industrial Applications
For many industries, the quality of water used in processes can significantly impact the final product. **Ultra pure water** is essential for industries such as pharmaceuticals, electronics, and food and beverage, where even the slightest impurity can lead to defects or health risks.
2.1. Industries That Benefit from Ultra Pure Water
Various sectors utilize ultra pure water equipment to enhance their operations. The **pharmaceutical industry**, for example, relies on ultra pure water for drug formulation and manufacturing. Similarly, the **electronics industry** uses ultra pure water in semiconductor manufacturing, where contaminants can compromise high-tech devices.
2.2. Role of Ultra Pure Water in Compliance and Safety
Maintaining compliance with regulatory standards is another significant benefit of ultra pure water systems. By utilizing such equipment, companies can ensure their processes meet health and safety regulations, ultimately protecting consumers and enhancing brand reputation.
3. Types of Ultra Pure Water Equipment
Understanding the different types of ultra pure water equipment is essential for selecting the right system for your industrial needs.
3.1. Reverse Osmosis Systems
**Reverse osmosis (RO) systems** are widely used for producing ultra pure water. They function by pushing water through a semi-permeable membrane, effectively removing dissolved solids, bacteria, and other contaminants. This technology is known for its ability to produce high-quality water with minimal energy consumption.
3.2. Deionization Units
**Deionization (DI) units** utilize ion exchange resins to remove charged particles from the water. This process is critical for applications requiring extremely low conductivity levels, such as laboratory experiments and high-tech manufacturing.
3.3. Ultraviolet (UV) Treatment Systems
**Ultraviolet treatment systems** are employed to disinfect water by using UV light to kill microorganisms. This method is crucial in industries where biological contaminants pose a significant risk, such as in food and beverage production.
4. Advantages of Using Ultra Pure Water Equipment
Investing in ultra pure water equipment brings numerous advantages that can enhance overall operational efficiency.
4.1. Enhanced Product Quality
Utilizing ultra pure water ensures that the final product meets the highest quality standards. The elimination of contaminants leads to fewer defects, higher yield rates, and ultimately greater customer satisfaction.
4.2. Increased Operational Efficiency
With ultra pure water systems, companies can streamline their processes. High-quality water reduces the risk of equipment fouling and corrosion, leading to less downtime and maintenance, thereby enhancing overall productivity.
4.3. Cost Savings in the Long Run
Although the initial investment in ultra pure water equipment may seem high, the long-term cost savings often outweigh the upfront expenses. Improved product quality and reduced maintenance costs translate to a better return on investment over time.
5. Selecting the Right Ultra Pure Water Equipment
Choosing the appropriate ultra pure water equipment is paramount for meeting specific industrial needs.
5.1. Assessing Your Water Quality Needs
Before selecting a system, it’s essential to assess the specific water quality requirements for your application. Analyzing the source water and determining the required purity levels will guide you in selecting the right equipment.
5.2. Evaluating System Compatibility and Future Scalability
Consider how the new system will integrate with existing processes. Additionally, evaluate whether the system can accommodate future growth as production demands change.
6. Installation and Maintenance Considerations
Proper installation and maintenance are critical for the longevity and efficiency of ultra pure water equipment.
6.1. Key Installation Tips
When installing ultra pure water systems, ensure that all components are correctly aligned and that there is adequate space for maintenance access. Consulting with experienced professionals can greatly assist in this process.
6.2. Regular Maintenance Best Practices
Routine maintenance is essential to ensure the system operates at peak efficiency. This includes regular cleaning, monitoring of water quality, and timely replacement of filters and membranes.
7. Case Studies: Success Stories in Ultra Pure Water Implementation
Examining real-life applications of ultra pure water equipment can provide valuable insights. For instance, a large pharmaceutical firm implemented a reverse osmosis system which resulted in a 30% reduction in production defects and considerable cost savings due to decreased downtime.
In another case, a semiconductor manufacturer upgraded their deionization units, which resulted in a 40% improvement in water quality, directly impacting their product yield and customer satisfaction levels.
8. Frequently Asked Questions
**Q1: What is the main advantage of using ultra pure water equipment?**
A1: The primary advantage is that it ensures the highest quality water for industrial processes, which significantly enhances product quality and reduces operational issues.
**Q2: How does reverse osmosis work?**
A2: Reverse osmosis works by forcing water through a semipermeable membrane that filters out impurities and contaminants, producing ultra pure water.
**Q3: Is maintenance challenging for ultra pure water systems?**
A3: While maintenance is necessary, following best practices and schedules can simplify the process and enhance system longevity.
**Q4: Can ultra pure water equipment be customized?**
A4: Yes, many manufacturers offer customizable solutions tailored to specific industry needs and water quality requirements.
**Q5: What industries primarily use ultra pure water?**
A5: Key industries include pharmaceuticals, electronics, food and beverage, and laboratories.
9. Conclusion
In the fast-paced world of industrial applications, **ultra pure water equipment** stands out as a crucial investment for companies striving for excellence. By ensuring that water meets the highest standards of purity, businesses can enhance product quality, increase operational efficiency, and ultimately achieve long-term cost savings. As industries continue to evolve, the role of ultra pure water equipment will only grow, making it essential for organizations to stay informed and equipped for the challenges ahead.
RELATED NEWS
Tel:
E-mail:
Ask For A Quick Quote
We will contact you within one working day. Please pay attention to your email